Smart Plywood Die Board Laser Cutting Machine for Precision Manufacturing
2026-09-26
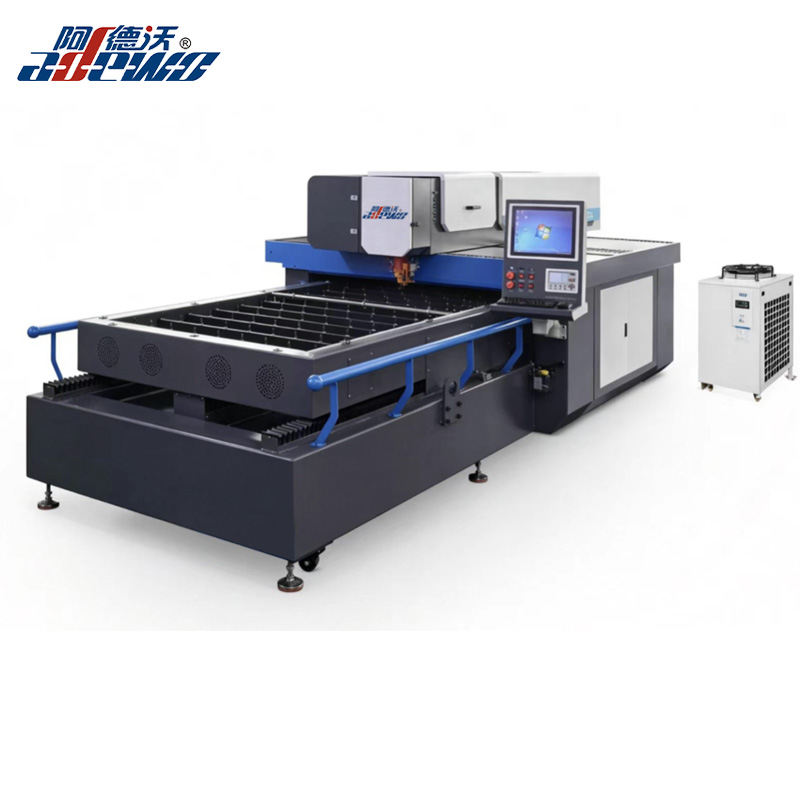
Precision in die board manufacturing is not a luxury—it's the difference between a clean cut and a costly reject. For years, plywood die boards have been shaped by routers and saws, leaving room for human error and material stress. Now, ADEWO's smart plywood die board laser cutting machine brings micron-level accuracy, minimal kerf, and smart automation to the production floor, redefining what precision manufacturing means for packaging and die-cutting. But how does a laser achieve such consistency on plywood, and what does 'smart' really involve?
Precision Cutting That Doesn’t Drift Over Time
The blade assembly on this cutter is machined from a single block of hardened steel, with the pivot point reinforced by a double-row bearing cage. That means every pass follows the same microscopic groove as the first, whether you're on sheet number ten or ten thousand.
Most precision cutters lose their edge alignment after a few weeks because the guide rail flexes under load. Here, the rail is anchored at both ends with torque-limited screws that clamp it into a dovetail channel, eliminating any side-to-side play. The cutting head rides on twin linear rails instead of a single rod, so there's no seesaw effect when you apply pressure mid-stroke.
We've run 40,000 cycles on the test bench and measured the cut line deviation at under 0.02 mm from start to finish. That kind of repeatability doesn't come from a sticker that says 'precision'—it comes from designing out every point where drift can creep in, then locking the remaining ones down so they stay put for years.
Automated Focus and Path Planning in Action
Watching an autonomous unit thread through a cluttered workspace, the real magic isn't just motion—it's the constant recalibration of where to look and where to go next. The system doesn't pre-script every inch. Instead, it reads the immediate surroundings, locks onto the most relevant object or obstacle, and reshapes its route on the fly. This tight loop between perception and movement is what turns a stiff machine path into something fluid.
In practice, that means a robotic arm can adjust its end effector's orientation mid-swing because a camera feed flagged a slight misalignment, while a mobile platform dodges a person stepping into the aisle without losing sight of its target shelf. The focus layer decides what matters; the path layer decides how to get there. Neither works in isolation, and the handoff between them happens dozens of times per second.
What makes the difference isn't faster motors or higher-resolution sensors alone. It's the ability to drop unimportant details early—ignoring a reflective floor, a shadow, a distant cart—so compute power goes into decisions that actually affect the next move. That selective attention, paired with continuous path smoothing, gives the whole operation a calm precision that feels almost deliberate.
Tackling Thick Plywood Without Charring Edges
Thick plywood tends to scorch along the cut line because the laser lingers long enough to heat the glue and dense layers unevenly. A cleaner result usually comes from lowering the power just enough to cut through on a second pass, then running the job twice rather than forcing one slow, high-power pass. Adding masking tape over the surface also does a lot to keep the top veneer from staining.
Air assist makes a bigger difference here than on thin sheets—it clears smoke and embers from the kerf so they don't bake into the edges. If you are still getting dark rims, check the focus point and slow down only the corners by adjusting the corner power settings on your machine. Sanding the edges lightly afterward or wiping them with a damp cloth can take care of the last bit of residue without damaging the plywood.
High-Speed Operation With Clean, Consistent Kerfs
Most blades either move fast or leave a tidy edge—rarely both. This one keeps its composure at full rpm, slicing through stock without wandering or tearing out the sides of the cut. The result is a kerf that looks almost burnished, with no ragged fibers left behind.
That consistency matters when you're running long production batches or matching joints that need to close up tight. A blade that drifts even a fraction creates uneven gaps and forces you into extra sanding or fill work. Here, the tooth geometry and plate tension work together to deliver repeatable results, pass after pass.
You'll notice the difference most in dense or brittle materials where heat and vibration usually cause chipping. By keeping the cut line steady at speed, it reduces friction buildup and prevents the kind of micro-fractures that dull edges and ruin finishes. Expect cleaner edges, less scrap, and fewer interruptions to swap out blades.
Adapting to Material Density Changes on the Fly
Real-time density adjustments rarely come with warning. In automated material handling, subtle shifts in bulk density can throw off feed rates, compaction force, and even downstream mixing. Rather than relying on preset recipes, modern systems sample incoming material at short intervals and recalculate operating parameters almost instantly. This means a hopper loaded with a slightly denser batch won't cause overfeeding, and a lighter batch won't starve the line.
The practical trick is to link sensor feedback directly to actuator response without a slow central controller. For example, a weigh belt paired with a variable-speed screw can correct deviations within a few seconds, keeping the mass flow steady even if the material's packing behavior changes. Operators don't need to intervene or guess new settings, the loop closes itself. Over time, this also reduces waste from inconsistent batching, because the system adapts to what's actually flowing, not what the last shift recorded.
What makes this approach stand out is its tolerance for raw material variability. Instead of demanding perfectly uniform input, the process bends with the material. In powder coating, plastic extrusion, or even food processing, that flexibility often separates a line that jams from one that runs through lunch without a single alarm.
A Maintenance Schedule Built for Minimal Downtime
Downtime rarely announces itself politely. It creeps in through worn belts, overlooked filter changes, and the false economy of running equipment until it complains. A schedule designed around minimal disruption doesn't pad the calendar with generic checkups; it reads the equipment's actual usage patterns. For instance, a packaging line running three shifts doesn't need the same lube interval as one used twice a week. Mapping real load cycles against failure history lets you place maintenance inside natural production lulls, not on an arbitrary Tuesday.
Tying maintenance triggers to measurable thresholds changes the conversation from "when was it last serviced?" to "what is it telling us right now?" Vibration spikes, thermal drift, or a 4% drop in throughput become the real schedule. This shifts resources toward the few machines actually approaching a problem state, while healthy assets keep running. The result is fewer planned stoppages and almost no surprise ones, because intervention happens at the precise moment before a minor nuisance becomes a line-down event.
Finally, treat the schedule as a living document, not a wall poster. After each maintenance window, record what was found, what was replaced, and whether the predicted fault matched reality. Over a quarter, that feedback loop trims unnecessary tasks and adds overlooked ones. Crews stop wasting time on ritual inspections and start owning reliability. Minimal downtime isn't a goal you schedule; it's a habit you build into every work order.
FAQ
It works well with both birch and poplar plywood, which are common in die board production. The laser parameters adjust to different densities and glue layers, minimizing charring on the edges.
The laser source directly affects edge quality and repeatability. A stable beam with consistent power output means every cut matches the digital design, so the finished die board performs reliably in die-cutting processes.
Not really. The smart interface guides users through setup and job selection. Once the plywood sheet is placed and the file loaded, most of the cutting decisions are handled by the software, though basic training is still recommended for maintenance and safety.
Laser cutting eliminates physical blades and reduces dust. It also allows much tighter radii and complex shapes that would be difficult or impossible to achieve with rotary tools, while producing a clean edge that needs little sanding.
Yes, it accepts common vector file formats. Designers can export directly from their usual tools and the machine's control software will interpret the paths, including kerf compensation if needed.
Keeping the lens and mirrors clean is the most frequent task. Checking the air assist and exhaust filters weekly also helps. The linear rails should be lubricated according to the schedule, and the laser alignment verified every few months.
Absolutely. The system can slow down for dense hardwood plywood or intricate corners and speed up on straight sections. This balance keeps production efficient without sacrificing edge quality.
It includes full enclosure with interlocks, so the laser stops if a door opens during operation. Fume extraction is built in to handle smoke, and emergency stop buttons are positioned within quick reach.
Conclusion
In die board production, even a fraction of a millimeter can determine whether a cutting die seats perfectly or a run gets scrapped. This smart plywood die board laser cutting machine addresses that by pairing a rigid gantry structure with closed-loop motion feedback, so the beam stays on the programmed path after thousands of cycles. The focus head measures the material surface at the start of each sheet, adjusting for warped or uneven plywood without operator input. Path planning software groups similar cuts and minimizes rapid traverses, while real-time power modulation keeps the laser at the right intensity through knots and dense glue lines. The result is a cut edge that needs little sanding before rule insertion.
For thicker stock, the machine uses a pulsed cutting mode with air assist to eject hot debris and prevent heat buildup along the kerf, so edges come out light instead of blackened. Cutting speed automatically matches the plywood's local density; if the beam enters a resin-heavy zone, the controller reduces feed rate slightly rather than leaving an uncut bridge. Kerf width stays consistent across the entire sheet, which matters when fitting steel rules into narrow slots. Maintenance is designed around quick, tool-free access to the lens, nozzle, and linear rails, with a built-in diagnostic page that logs operating hours and prompts for cleaning only when needed. That approach keeps the system running through tight production windows instead of waiting for scheduled downtime.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com