Sanding Disc Company Guide to Choosing the Right Abrasive Discs
2026-10-09
Most sanding disc guides read like spec sheets—dry, generic, and useless when you’re staring at a half-finished job. This one takes a different route. You’ll learn which abrasive type, grit, and backing actually hold up on metal, wood, or composite, and why cheap discs cost more in the long run. We’ve leaned on real-world testing and insights from SHENZHEN SUN ABRASIVES to give you practical selection criteria you can use today. Ready to stop guessing and start sanding smarter?
Your Abrasive Grain Choice Is the Real Starting Point
Most grinding problems don't start with the machine settings or the bond type—they begin at the grain level. The abrasive grain you pick determines how the wheel cuts, how heat builds up, and how long the tool actually lasts. Yet too many shops treat grain selection as an afterthought, grabbing whatever is on the shelf and then wondering why the finish is inconsistent or the cycle time keeps creeping up.
Think about what the grain is really doing: each particle is a tiny cutting edge, and the shape, hardness, and friability of that edge directly control material removal. A tough, blocky grain like zirconia alumina will hold up under heavy pressure but might not give you the sharpness needed for a fine finish. A friable ceramic grain fractures constantly, exposing fresh edges and running cooler, but it can break down too fast on soft materials. Matching the grain to the workpiece—not the other way around—is where real gains hide.
Before you adjust speeds, feeds, or dressing intervals, stop and ask what the grain itself is contributing. A cheap grain that dulls quickly forces you to compensate with more pressure, more heat, and more downtime. A well-chosen grain can reduce dressing frequency, improve form holding, and lower total cost per part even if the wheel costs more upfront. That's why the abrasive grain isn't just one variable among many—it's the foundation everything else builds on.
Backing Weight Is the Spec Nobody Checks Until It's Too Late
Most people picking out carpet zero in on face weight, fiber type, or color, but almost nobody asks about the backing weight. That overlooked number is often what determines whether a carpet holds up in a busy hallway or starts to stretch, wrinkle, and split at the seams. A too-light backing can fail within months of installation, but by the time you notice, the warranty window has already closed.
There's an old industry saying: a carpet is only as good as its back. Plenty of low-bid products cut corners exactly here, using flimsy secondary backings to shave cost without changing the look of the sample. Nobody checks this spec during procurement, so the problem stays hidden until the carpet starts bunching up like an old bedsheet in the corridor. By then, the repair bill eats up whatever was saved on the front end.
Instead of waiting for a failure, glance at the backing weight on the spec sheet—especially for commercial spaces or homes with pets and heavy foot traffic. It won't be the flashiest number on the page, but it will tell you more about real-world durability than any stain warranty. Don't be the person who checks it only after the carpet has already given up.
Grit Numbers Lie More Than You'd Expect
The number printed on a sheet of sandpaper feels precise, but it hides a lot of variation. Two brands can both label a product 220 grit, yet one cuts like 180 and the other burnishes like 320 because the actual particle size distribution is allowed to drift. Abrasive manufacturers don't all use the same grading standards, and even within a single standard, the tolerance band is wide enough to change how the paper behaves on wood.
Then there's the abrasive material itself. Aluminum oxide, silicon carbide, ceramic, and garnet all behave differently at the same grit number—some fracture to expose fresh edges, others dull quickly. The backing and bond strength also matter more than the number suggests. A cheap 400-grit paper might leave deeper scratches than a quality 320-grit sheet simply because the particles aren't bonded as firmly and roll around under pressure. So if you're chasing a specific surface finish, relying on the printed grit alone will mislead you more often than not.
Why Hole Patterns Make or Break Dust Control
Dust doesn't behave like a single drifting cloud—it hugs surfaces, swirls in eddies, and slips through whatever gaps the airflow allows. The hole pattern on a dust-control cover or screen essentially dictates where suction reaches and where it doesn't. Clustered perforations may look aggressive, but they often starve the outer edges of airflow, leaving fine particles to escape along the perimeter. In contrast, evenly spaced holes with slight edge offset create a more uniform pressure drop, pulling dust inward before it can scatter.
Another overlooked factor is hole geometry and orientation. Round holes tend to clog less under fibrous dust, while angled or louvered openings can redirect incoming air across the surface, sweeping settled particles toward the extraction zone. A pattern that's too dense weakens the panel and causes whistling; too sparse creates dead zones where dust accumulates unnoticed. The spacing-to-diameter ratio matters more than the total open area, because turbulence near each opening can either trap or release fine material depending on how closely the holes interact.
Field experience shows that swapping a randomly drilled plate for a staggered, slightly countersunk pattern can cut visible dust escape by half without increasing fan power. That's because the pattern itself acts as a passive flow conditioner, breaking up high-velocity jets and spreading negative pressure across the whole face. When hole patterns are treated as an afterthought, even well-designed hoods and filters underperform—proof that small geometric decisions ripple through the entire dust-control system.
Flexible, Stiff, or Flap? The Shape You Pick Changes Everything
Most people assume the material alone decides how an object behaves. But the shape you choose—whether it flexes under pressure, holds rigid, or flaps loosely—has an even bigger say. A flexible profile bends to absorb sudden force, then springs back without cracking. A stiff one transfers every bit of energy straight through, leaving no room for give. And a flapping edge? That creates drag, flutter, and unpredictable motion that can either stabilize or destabilize the whole setup.
Think of a thin sheet in the wind. Hold it flat and rigid, and it catches the air like a sail, pulling hard. Let the trailing edge go soft, and it starts to ripple, shedding load in pulses. Give the whole thing a slight curve that flexes, and it tunes itself to the airflow, finding a balance no fixed shape could match. The difference isn't subtle—it's the difference between snapping under a gust and riding it out.
That's why choosing a shape isn't just about looks or feel. It's about matching the structure to the specific stresses it will meet. Pick a stiff form where you need precision and feedback. Pick a flexible one where you need recovery and shock absorption. Pick a flapping design only if you understand the chaos it introduces. The wrong choice can turn a promising design into a frustrating failure.
Cheap Discs Often Cost You More by the End of the Job
It starts innocently enough. You grab a stack of budget grinding discs because the price per unit looks unbeatable on the shelf. But once you're out in the field, the real math kicks in. The abrasive wears down unevenly, you're swapping discs every few minutes, and the constant pressure you have to apply slows your stroke to a crawl. What felt like a bargain at the checkout becomes a slow bleed of time and labor.
Then there's the hidden damage. Low-cost discs often shed grit unpredictably or glaze over mid-cut, forcing you to bear down just to keep the tool biting. That extra heat and vibration doesn't just kill the disc faster — it transfers straight into your grinder's bearings and gearbox. A few jobs later, you're replacing a tool that should have lasted years, all because the consumable couldn't hold its edge.
Quality abrasives aren't about paying for a logo. They're engineered with controlled grain spacing and stronger bonding agents so they cut cleaner, run cooler, and wear at a predictable rate. When you do the final tally on time saved, fewer change-outs, and less wear on your equipment, the cheaper disc almost always ends up costing more by the end of the job — and then some.
FAQ
Start with the material you're sanding. Harder surfaces like metal or hardwood typically need a tougher abrasive such as zirconia or ceramic, while softer materials like aluminum or paint often work better with aluminum oxide. Also note the grit range: lower grits remove stock fast, higher grits leave a smoother finish.
Fiber backing holds up well on aggressive grinding and high-pressure work, while cloth or film backings flex more and are better for contoured surfaces or fine finishing. Plastic backings can bridge the gap when you need some rigidity without excessive heat buildup.
Use an open-coat disc with a stearate or anti-loading coating. These features create space for swarf to escape and reduce buildup. Also match grit carefully: too fine a grit on soft material tends to clog quickly.
Move to a flap disc when you need both stock removal and a decent finish in one step, or when the workpiece is thinner and can't handle the aggressive cut of a grinding wheel. Flap discs also run cooler and leave fewer deep scratches if you maintain a steady angle.
Grit size refers to the abrasive particle size. Lower numbers like 24 or 36 cut aggressively and are best for heavy material removal or weld blending. Mid-range grits like 60 or 80 balance cutting and finishing. Higher grits from 120 up refine scratches and prepare surfaces for paint or coating.
You can, but stainless steel often benefits from a disc labeled for stainless or INOX use. These discs usually have additives that reduce heat discoloration and contamination. Carbon steel is more forgiving, but a disc designed for stainless will still work well on it.
If the disc glazes over, stalls the tool, or leaves burn marks on the workpiece, you are pressing too hard. Let the abrasive do the cutting. Use just enough pressure to keep the disc engaged without bogging down the tool, and check that your RPM matches the disc's rating.
Conclusion
Most people reach for a sanding disc based on grit alone, but the actual performance starts much earlier with the abrasive grain. Ceramic alumina, zirconia, and aluminum oxide each break down differently under heat and pressure, so matching the grain to your material—whether it’s hardwood, softwood, metal, or composite—shapes how fast you cut and how long the disc stays sharp. Backing weight is another spec that rarely gets checked until a disc rips apart mid-sand or loses its edge prematurely. A heavier backing, usually rated from A to F, gives you more tear resistance and better support for aggressive grinding, while a lighter backing flexes more but won’t survive rough edges or high-pressure work. And grit numbers? They’re not as reliable as the label suggests. Two discs marked 80 grit from different makers can leave noticeably different scratch patterns because the actual particle size distribution and binder formulation vary. It’s worth testing a few brands on scrap before committing to a whole box.
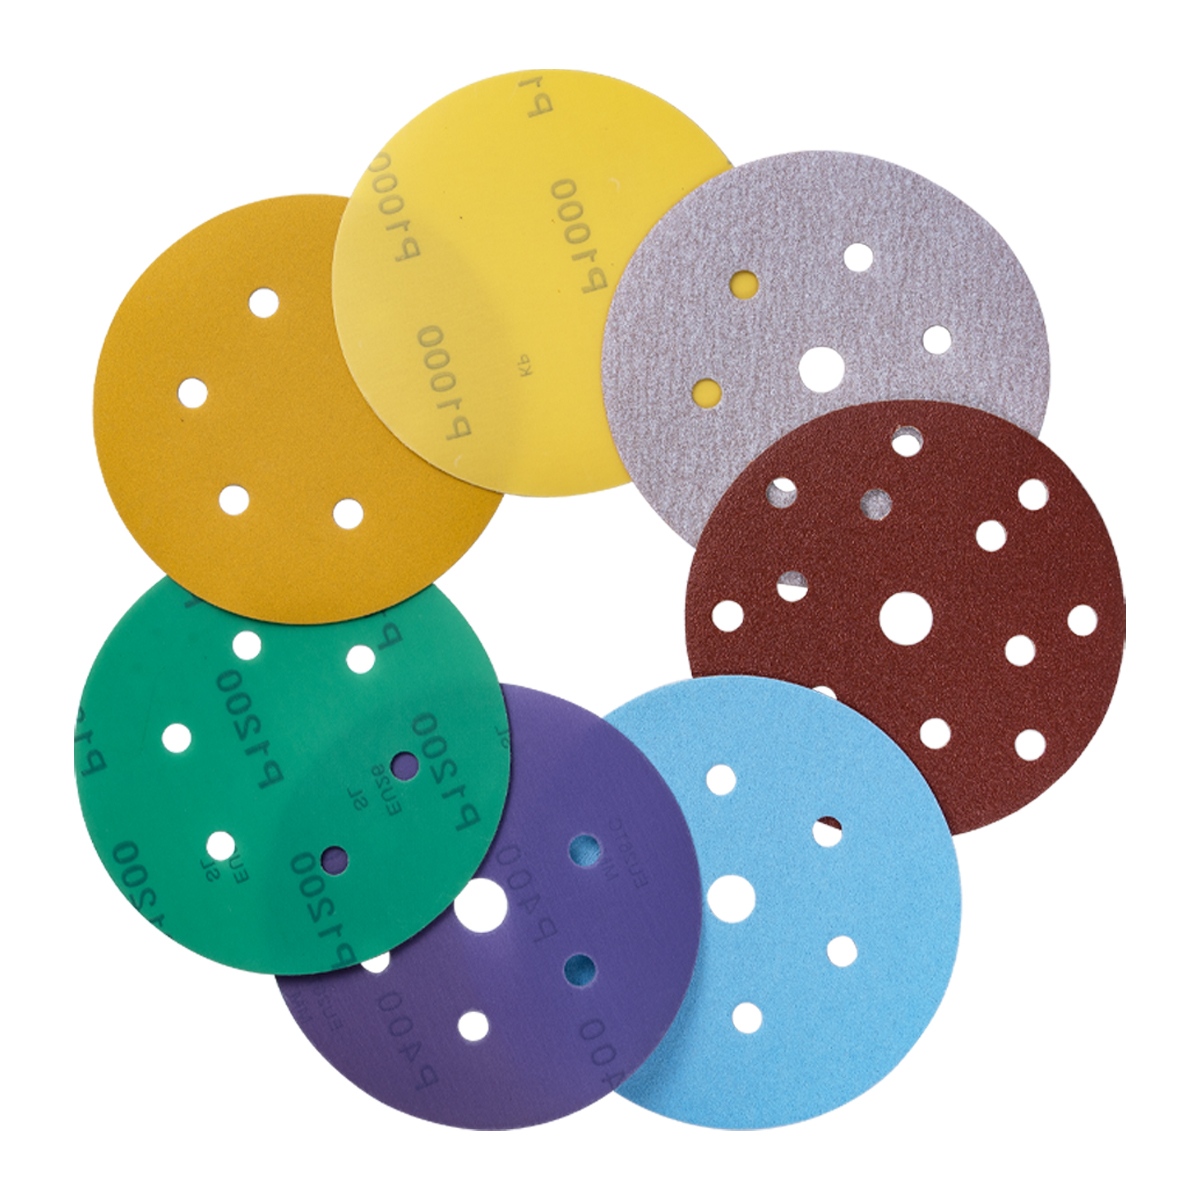
The hole pattern on a disc isn’t just cosmetic—it directly controls dust evacuation, heat buildup, and how long the abrasive keeps cutting. Mismatched holes between your backing pad and disc mean dust packs into the gaps, which clogs the grain and can scorch the surface. If you’re switching between brands, double-check that the hole arrangement lines up exactly, not just the diameter. Then there’s the shape: stiff fiber discs are great for weld blending and heavy stock removal, flexible PSA discs follow contours without gouging, and flap discs handle both grinding and finishing in one step. Choosing the wrong flex or backing style for your grinder and workpiece often leads to uneven wear, swirl marks, or premature loading. Finally, cheap discs rarely save money. They may use inconsistent grain distribution, thin backing, or weak resins, so you burn through more discs, spend more time swapping them, and risk rework from uneven scratches. A slightly pricier disc that holds its edge longer and cuts cooler usually costs less per square foot by the end of the job.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn