Empty Tube Factory: A Complete Guide to How Tubes Are Made
2026-08-20
Ever wondered how the humble empty tube that holds your toothpaste, ointment, or cosmetics comes into existence? Behind every perfectly sealed, ready-to-fill tube lies a fascinating journey of precision engineering and material science. In this complete guide, we pull back the curtain on the tube manufacturing process—from raw material selection to the final quality checks. Whether you're a brand owner sourcing packaging or simply curious about everyday objects, you'll discover the intricate steps that turn flat sheets and granules into the sleek, functional tubes you see on shelves. And when it comes to mastering this craft, few names carry the expertise of Sanrong Packaging, a leader in delivering high-quality tube solutions worldwide. Let’s dive into the world of empty tube factories and uncover what truly goes into making a tube that stands out.
What really happens between raw pellets and a finished empty tube?
Raw pellets don't simply melt—they get progressively compressed and sheared along a heated screw. The barrel zones are tuned so the polymer transitions from solid granules to a dense, bubble-free melt without burning the outer layer. That back pressure is what forces out trapped volatiles and keeps wall thickness steady later on.
Once the melt passes the screen pack and enters the die head, the mandrel and die lip set the initial tube geometry. But the parison is still soft, so draw-down and die swell have to be countered by a slight oversize gap. The moment it leaves the die, it hits the vacuum calibrator where cold water freezes the outside diameter while air pressure holds the still-molten inner wall against a series of sizing sleeves.
From there, it's a continuous pull through spray baths and a caterpillar haul-off. Laser micrometers check diameter and wall thickness in real time, and any drift triggers automatic adjustments to screw speed or haul-off tension. Only after the tube passes those checks does the flying saw cut it into lengths—leaving a finished empty tube that looks simple but is actually a tightly controlled thermal and mechanical process.
The forming process that gives a tube body its squeeze and bounce
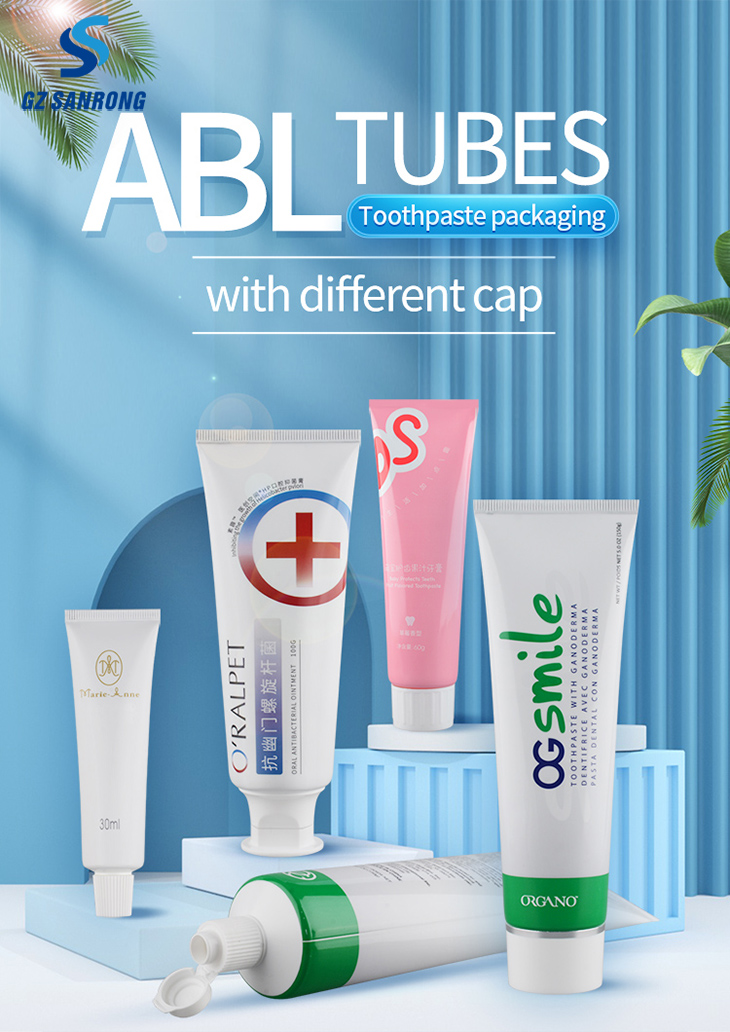
Most tube bodies start as a multilayered parison, coextruded from a blend of polyethylene grades so the inner layer stays chemically inert while the outer layer takes the mechanical load. During blow molding, the parison is inflated against a chilled cavity with precisely staged air pressure. The rapid expansion stretches polymer chains around the circumference, aligning them enough to create a memory effect: when you squeeze the tube, those oriented chains want to return to their inflated diameter, which produces the bounce. At the same time, the axial direction cools more slowly, leaving enough slack for easy compression without cracking.
Wall thickness is tuned by varying the die gap during extrusion, with the shoulder and crimp area kept slightly thicker for crack resistance and the mid-body thinned to lower squeeze force. Some lines use a water-cooled mandrel to set the inner diameter before the outer skin freezes, locking in a smooth bore that reduces product hang-up and improves recovery after repeated flexing. Minor amounts of elastomer or a low-density fraction in the outer layer soften the initial hand feel, while a higher-density core acts as the spring, giving the tube a controlled rebound rather than a limp collapse.
Why shoulder shape and cap torque decide whether a tube leaks or survives
The shoulder profile dictates where the seal actually lives under load. A generous radius spreads contact pressure across a wider band, letting the gasket settle into a stable groove. A sharp or uneven shoulder, by contrast, forces that same pressure into a narrow ring—often at the edge of the mating surface—where micro-channels can open once the assembly relaxes.
Cap torque sets the stage but doesn't finish the job alone. Too little torque leaves the shoulder under-engaged, so the seal never reaches its designed compression set. Too much torque and the shoulder deforms or the thread strips, creating a false sense of security right up until the first pressure cycle. The sweet spot is often narrower than most assembly instructions admit.
What decides between a leak and a long service life is the interaction: a well-shaped shoulder lets torque translate into uniform preload, while a poor shape turns even correct torque into localized stress. Inspecting for leaks after the fact usually points back to one of these two variables—either the geometry couldn't distribute the load, or the torque couldn't hold the geometry in place.
How printing and varnish keep tube artwork from flaking off in use
On collapsible tubes, artwork survival depends on more than just a tough ink. The base polymer—often polyethylene or a laminate—has low surface energy, so converters first treat the surface with corona discharge or a thin primer to give the ink something to grip. Without that step, even the best-cured ink can peel away after a few squeezes.
The ink system itself is usually UV-cured and formulated to flex with the tube walls rather than crack under repeated rolling and flattening. After the design is laid down, a clear varnish is applied as the final layer. This varnish does the heavy lifting in daily use: it resists abrasion from hands and countertops, blocks oils and toothpaste residue, and spreads mechanical stress so the printed layer beneath stays intact instead of flaking off at fold lines.
Low-gloss or matte varnishes can also reduce the visibility of micro-scratches, keeping the tube looking cleaner longer. The result is that the artwork remains legible and attached through the whole life of the product, from first open to the last squeeze.
The pressure tests and drop checks a tube must pass before leaving the floor
Every tube gets a hydrostatic test before it can be tagged for shipment. The line is capped and filled with water, then pressurized to at least 1.5 times the working pressure called for in the order. The pressure holds for a minimum of ten seconds while inspectors watch for any weeping at the weld seam or a sudden drop on the calibrated gauge. If the water temperature is below 5°C, the test is delayed because cold metal can mask hairline cracks that would open up later in service.
Drop checks are just as unforgiving. A tube is lifted to a height that depends on its diameter and wall thickness, then released onto a steel plate. After the impact, the ends and body get a close visual inspection for dents, splits, or any loss of roundness. Some orders also require a Charpy impact test on a sample cut from the same heat to prove the steel won't turn brittle in cold weather. These checks mimic what happens when a bundle shifts during trucking or a pipe slips off a forklift on a job site.
None of this is done on a sampling basis. Every single tube goes through the full sequence, and the results are written down on the mill sheet that travels with the order. If a tube fails either the pressure test or the drop check, it is set aside for rework or scrap, never re-tested and passed. That is why the tubes that do leave the floor can be trusted to handle high-pressure lines, structural loads, and rough handling without failing unexpectedly.
What to look for in an empty tube factory before you commit to a supplier
A clean showroom tells you very little. Walk the production floor and watch how raw resin moves through extrusion, printing, capping, and sealing. Ask about machine age, maintenance logs, and unplanned downtime for the lines that would handle your order. A factory that hesitates to show you this side of the operation is already giving you an answer.
Material consistency matters more than a sample on a desk. Request batch records for wall thickness, shoulder strength, and seal integrity over the last six months, not just the best run. If they use recycled content, ask how it is sourced and tested. For cosmetic or pharmaceutical tubes, insist on migration and compatibility data with your specific formula.
Flexibility shows up before you sign. Give them a small trial order with a tight turnaround and a color change request. See how they communicate when a specification shifts mid-production. Ask about minimum order quantities, buffer stock for repeat orders, and what happens if a shipment is short or delayed. These small tests reveal more than any audit checklist.
FAQ
Most factories work with aluminum, polyethylene, or laminate blends. Aluminum offers strong barrier properties, while plastic tubes are lighter and cheaper to ship. Laminates let you combine layers for better protection against oxygen or moisture.
For plastic tubes, resin pellets are melted and pushed through an extruder to create a continuous hollow sleeve, which is then cut to length. Aluminum tubes start as slugs that get impact-extruded into shape under high pressure, then trimmed and cleaned.
The coating prevents the product from reacting with the tube material. For example, fluoride toothpaste can corrode bare aluminum, so a thin epoxy lining is sprayed inside and cured to keep the formula stable.
Tubes pass through rotary offset or flexographic printers that apply up to five or six colors in one pass. After printing, a clear varnish or matte finish is often added to protect the artwork from scratches and moisture.
For plastic tubes, the shoulder is usually injection-molded directly onto the tube body, creating a strong seal. Aluminum tubes often get a separate plastic shoulder that is crimped or screwed on. The cap is then applied, either as a flip-top or a screw closure.
Factories run burst tests, squeeze tests, and vacuum tests. A tube is filled with air or water, sealed, and subjected to pressure until it fails. They also check the crimp or seal area for pinholes by submerging the tube in water and looking for bubbles.
It depends on the material. Aluminum tubes are widely recyclable if they are empty and clean. Plastic tubes are trickier because the multi-layer laminate and shoulder materials need to be separated, though mono-material polyethylene tubes are becoming more common to improve recyclability.
Conclusion
Turning raw plastic pellets into a dependable empty tube involves far more than melting and molding. The pellets are first extruded into a continuous sleeve, then cut and shaped through a forming process that determines how the finished tube feels when squeezed and how quickly it springs back. A poorly formed body might feel flat or crack at the crease, so factories pay close attention to wall thickness and material distribution. Just as important are the shoulder geometry and cap torque: a shoulder that is slightly off-angle or a cap that threads on too loosely can lead to slow leaks, product contamination, or caps that pop open during shipping. Coatings also play a silent but vital role. Printing and varnish are not just decorative; they form a protective layer that stops the artwork from flaking, scratching, or fading after repeated handling and squeezing.
Before any tube leaves the floor, it must survive a battery of pressure tests and drop checks that simulate real-world abuse, from being squeezed hard to falling off a shelf. Factories that skip these steps often ship tubes that look fine but fail in the field. When evaluating a potential supplier, look beyond the showroom samples. Ask how the factory controls wall thickness, what torque values they use for cap application, how they cure varnish, and whether they keep records of pressure-test failures. A trustworthy empty tube factory will be transparent about reject rates and willing to walk you through their entire process, from pellet drying and extrusion to final inspection. That level of openness is a stronger signal than any polished brochure, because it shows they understand that a tube is only as good as the weakest link in its production chain.
Contact Us
Contact Person: Alex Wu
Email: [email protected]
Tel/WhatsApp: 86-20-37965868
Website: https://www.gzsanrong.com/en.html