China Sanitary Ware Vertical Lift Plating Equipment: Key Benefits and Features
2026-10-02
Ever wondered how high-end sanitary ware achieves that flawless, mirror-like chrome finish? The secret often lies in vertical lift plating systems—and when it comes to trusted manufacturers in China, Junda stands out. In this post, we'll explore the key benefits and features that make this equipment a game-changer for production efficiency and product quality.
The Vertical Lift Advantage for Complex Sanitary Ware Geometries
Complex sanitary ware rarely rewards a simple parting line. The trapways, rim channels, and hidden cavities that define a modern toilet or basin create undercuts and deep recesses that would normally demand multiple side pulls or collapsible cores. A vertical lift axis turns many of these problem areas into straightforward draw directions. Instead of fighting the geometry from the side, the tool opens upward, letting the upper mold half clear the most intricate internal features while the casting stays seated in the lower half. Gravity assists the release, and the need for secondary moving components drops sharply.
This approach also cleans up the visible surface. Every slide or side action leaves a witness line or a slight mismatch on the finished piece. With vertical lift, the main parting line sits lower or follows an already existing contour, so the glazed surface stays uninterrupted where it matters most. Tooling becomes simpler to maintain because there are fewer wear-prone slides, and the mold can be built in a more compact footprint. For sanitary ware plants running multiple cavities, that space saving translates directly into higher output without expanding the line.
Cycle time benefits follow from the same logic. A vertical opening stroke is predictable and easy to automate, and stripping a complex shape along one axis often requires less force than pulling it through a side action. The casting ejects cleanly, reducing hand finishing and scrap. Designers gain freedom to push trapway shapes and rim contours further because the mold no longer dictates a compromise between geometry and demoldability. In pressure casting or conventional slip casting, the vertical lift advantage means fewer limits on what a sanitary ware form can be.
Cutting Floor Space Without Sacrificing Plating Quality
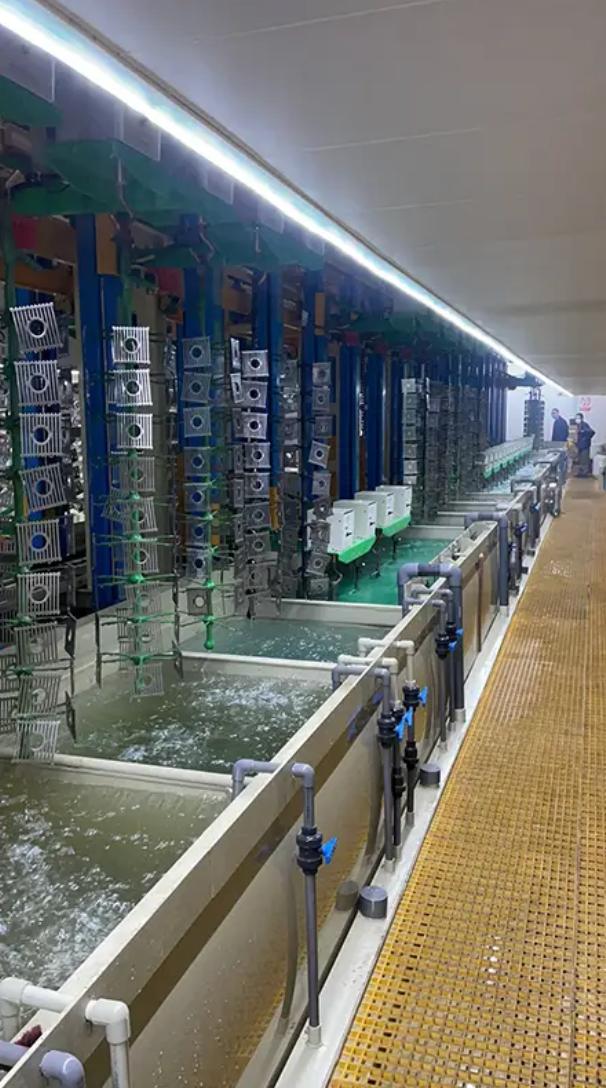
A smaller plating line doesn't have to mean a compromise on finish quality. By shifting to vertical hoist handling and arranging tanks in a U-shaped or multi-row configuration, facilities can often reclaim 20–30% of the floor area that a conventional straight-line setup would occupy. The key is keeping every step of the pre-treatment, plating, and rinsing sequence within a tightly controlled envelope so parts move quickly and exposure times stay consistent.
Quality in plating hinges less on tank footprint than on how well the solution flows around the part and how steady the electrical current remains. Narrow, deeper tanks fitted with eductor nozzles or air sparging can produce a more uniform deposit than wide, shallow baths where solution stagnates along the edges. Paired with pulse rectification, these compact cells handle complex geometries without the need for oversized anodes or extra buffer volume.
Automation also plays an underrated role in space reduction. A properly programmed hoist can pass through tighter aisle clearances than a person wheeling a rack, so adjacent lines can be placed closer together. Moving rectifiers, filters, and exhaust ducting to a mezzanine or rooftop skid frees up even more floor without disturbing the chemical balance of the baths.
How Controlled Immersion Rates Improve Chrome Adhesion
Getting chrome to stick isn't just about bath chemistry; how fast the part enters the solution matters just as much. A slow, steady immersion rate gives the current a chance to spread evenly across the surface before heavy deposition starts. Rush the entry and you're likely to see patchy coverage or, worse, plating that flakes off after a few thermal cycles.
When the workpiece goes in at a controlled rate, the chromium ions have time to form a thin, coherent initial layer. Those first few atomic layers set the tone for everything that follows. If the part plunges in too quickly, local current spikes and uneven nucleation create built-in stress points that weaken the bond later.
Many shops overlook this variable, but adjusting the immersion speed can clear up adhesion failures that no amount of cleaning or activation will fix. A controlled entry lets the interface between base metal and chrome build gradually, reducing trapped gas and improving bond strength. In practice, a constant rate of entry—often just a few millimeters per second—gives far more reliable results than hand-dipping or a quick dunk.
Reducing Chemical Drag-Out with Smart Lift Programming
Line speed and dwell time rarely get the attention they deserve when drag-out climbs. Instead of accepting a fixed withdrawal rate, smart lift programming adjusts the vertical travel profile to the part geometry and solution viscosity. Slowing the first few centimeters of lift lets the bulk of the liquid sheet break away and drain back into the tank, while a faster intermediate stroke keeps cycle time in check. This creates a two-stage or multi-stage pull that can cut chemical carryover by double digits without adding equipment.
The real advantage shows up on complex shapes. Pockets, blind holes, and sharp edges trap solution regardless of drain boards if the part leaves at a constant speed. By programming a brief pause just as the top edge clears the bath, trapped volumes get an extra moment to equalize and flow downward. Operators often report cleaner rinse tanks with no change to the chemistry itself, simply because less concentrated solution is leaving the process.
Implementation starts with recording current drag-out rates per rack or barrel, then testing lift curves in small increments. A ten percent reduction in withdrawal speed at the critical break point may add only a second or two to the line, but it can lower replenishment costs and sludge generation in waste treatment. Over a month of continuous plating or coating, that quiet adjustment in the PLC becomes one of the cheapest chemical savings available.
Built for High-Mix Production: Quick Changeovers and Flexibility
Instead of bolting down dedicated tooling for each product, the platform uses a snap-and-lock fixture system that positions parts without manual alignment. Operators simply swap the lightweight plates, and the controller loads the corresponding recipe—pressure, dwell time, feed rate—from internal memory. A full changeover between two completely different part geometries rarely exceeds four minutes, and no tools are required for the mechanical swap.
That same design carries over to the software side. The machine recognizes each new fixture via embedded RFID tags and automatically adjusts guide rails, sensor positions, and dispensing parameters to match the incoming product profile. Because the adjustments are driven by stored profiles rather than operator guesswork, a single line can bounce between a 12-piece prototype batch and a 500-piece validation run without any loss in placement accuracy.
The practical result is that high-mix schedules no longer punish you with downtime. Contract manufacturers can group small orders from different customers on the same afternoon shift, run them back-to-back, and still meet takt time. In one electronics assembly cell, the switch from a rigid changeover procedure to this flexible setup cut weekly changeover time by 71% while allowing the plant to take on three new low-volume customers without adding a second line.
From Manual Lines to Automated Vertical Systems: What Changes
Moving from manual lines to automated vertical systems flips the physical logic of a facility. Instead of spreading work across long horizontal conveyors or shelving rows, the process stacks upward, often reclaiming 60–80% of the floor area. Workers stop walking miles each shift to gather parts or orders—the goods travel down to them at a fixed ergonomic station. That single change cuts transit time sharply and turns what used to be a sprawling, movement-heavy layout into a compact, vertical cube where density and accessibility go hand in hand.
Labor changes too, but not in the way most fear. The old manual line rewarded speed and endurance: walking, reaching, counting, and repeating. An automated vertical system shifts the human role toward oversight—monitoring pick queues, handling exceptions, and managing replenishment. It’s less about physical effort and more about attention and system fluency. Some teams struggle with the transition because the skills look different on paper, yet the core need for dependable, alert workers never goes away.
Accuracy and pace stop depending on the fastest or most careful person on the line. The machine presents one item at a time, confirms each transaction, and logs inventory in real time. Error rates typically drop below 0.1%, and throughput becomes far more consistent across shifts. That consistency often reveals a hidden benefit: managers can finally plan around reliable cycle times instead of guessing how a tired crew might perform on a Friday afternoon.
FAQ
The vertical lift design handles large, contoured pieces like basins and toilets without the surface contact marks common in barrel plating. It also lets the parts enter and exit the bath at a controlled angle, which reduces air pockets and gives a more even deposit in deep recesses.
Instead of rotating or shaking parts, the vertical stroke moves them cleanly through each bath. This keeps current density stable across the surface and prevents the edge burning or shadowing you often see on highly curved sanitary fittings.
It is typically built for copper-nickel-chrome sequences on brass or ABS plastic substrates. Some configurations also handle satin nickel, gunmetal, or PVD top coats, depending on the pre-treatment and rectifier setup.
Chinese manufacturers offer a mature supply chain for plating tanks, rectifiers, and filtration components at lower cost. Many can also customize the line layout and automation level, and lead times are usually shorter because the supporting component network is already in place.
The equipment generally includes counterflow rinses, separate drainage for chromium and nickel streams, and fume extraction hoods around heated tanks. This lets the plating shop recover more chemistry and stay within discharge limits without adding a lot of external treatment capacity.
Look at the tank material thickness, whether rectifier cooling is air or water based, the type of anode baskets, and whether the PLC can store multiple plating recipes. A well-built line uses PP or PVC tanks, titanium heaters, and a frame that resists corrosion from mist.
Yes. Programmable hoists with position sensors and recipe management allow different part types to run back-to-back with minimal manual handling. That reduces cycle time and keeps the film thickness consistent from rack to rack.
Conclusion
Vertical lift plating equipment has become a practical answer for sanitary ware manufacturers dealing with intricate ceramic and metal forms. Unlike conventional barrel or horizontal lines, the vertical orientation lets parts enter baths at a controlled angle, which helps solution reach recessed areas that trap air or cause uneven deposits. This approach also compresses the line footprint, freeing up factory floor space without forcing operators to sacrifice thickness distribution or chrome brightness. The smooth, programmable lowering and raising of racks keeps immersion speed consistent, giving the chrome layer a better chance to bond tightly to the substrate and resist peeling at sharp edges or hidden curves.
Beyond geometry and adhesion, smart lift programming cuts chemical drag-out by pausing racks above tanks and tilting them just enough to let excess solution drain back before transfer. That means fewer bath contamination issues and lower replenishment costs. The equipment is also designed for high-mix production, with quick-change flight bars and recipe memory that let a line switch between faucet bodies, shower arms, and flush valve parts within minutes. For plants moving away from manual hoists, the shift to automated vertical systems brings repeatable cycle times, fewer operator errors, and better data logging for every rack processed. What used to depend on a skilled hand now runs with predictable results shift after shift.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com